Week 1 HW: Final Project Ideas
Biomanufacturing an Antimicrobial, Breathable Prosthetic Bio-Liner via In Situ Biotemplating
- Student: Juan Baquerizo (Active Global Contributor - Ecuador)
- Course: MAS.S65 / How to Biomanufacture (Almost) Anything (Fall 2026)
- Instructors: David Sun Kong, Ph.D., George Church, Joseph Jacobson
- Assignment: Homework #1 — Project Proposal
(1) What you would like to biomanufacture and why?
Target Output
The goal of this project is to biomanufacture a customized, antimicrobial, and breathable prosthetic socket bio-liner produced via in situ biotemplating inside customized 3D-printed molds (FDM).
The finished device is a seamless, elastomeric hydrogel sleeve composed of an ultra-pure bacterial cellulose (BC) nanofibrillar matrix, plasticized with medical-grade glycerol and surface-functionalized with recombinant antimicrobial peptides (AMPs).
Motivation and Clinical Importance
The prosthetic socket is the primary load-bearing mechanical interface connecting an amputee’s residual limb to their prosthetic hardware. Standard commercial liners rely almost universally on synthetic non-porous elastomers (silicone, polyurethane, or thermoplastic elastomer/TPE). While they provide cushioning, they introduce severe clinical complications:
- Maceration and Dermatitis: Synthetic elastomers are impermeable. In warm and humid climates—such as the equatorial regions of Ecuador—sweat remains trapped against the skin. This continuously macerates the stratum corneum, causing friction blisters, severe skin breakdown, and contact dermatitis.
- Recurrent Infections: Trapped moisture, mechanical friction, and elevated skin temperature create an ideal environment for pathogenic bacteria (Staphylococcus aureus, Pseudomonas aeruginosa). Dermal infections routinely force amputees to suspend prosthesis use for weeks or months.
- Prohibitive Cost and Accessibility: Commercial silicone liners cost between $300 and $1,200 USD each, require replacement every 6 to 12 months, and rely on fragile international supply chains. For public healthcare systems and amputees in developing countries, this recurring cost is unsustainable.
Bacterial cellulose offers a natural biological solution: it forms an ultra-pure, 3D nanofibrillar hydrogel network with high tensile strength, high fluid capacity, and intrinsic vapor permeability. By growing cellulose directly inside patient-matched molds (modeled from 3D scans and printed on desktop FDM printers) and functionalizing the matrix with recombinant AMPs, this project creates a customized, breathable, and infection-resistant interface tailored for decentralized manufacturing.
(2) What living system would you use?
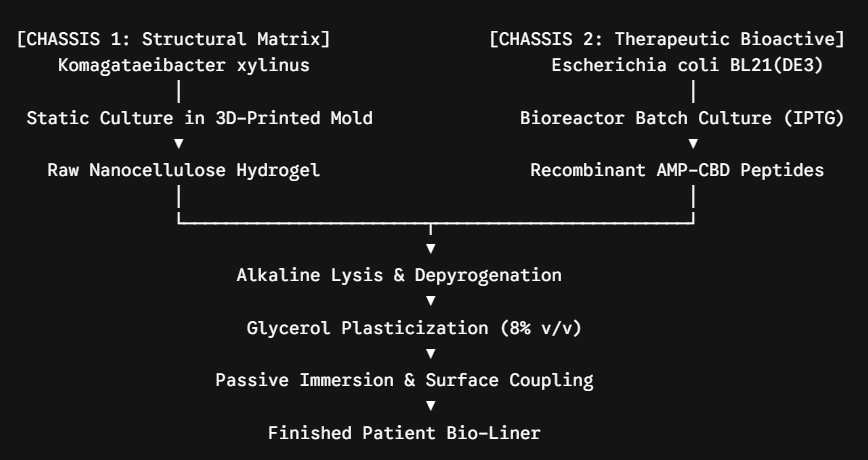
A modular biological architecture is used, splitting structural matrix synthesis from therapeutic biofunctionalization:
Living Chassis Selection
- Structural Chassis: Komagataeibacter xylinus (Gram-negative, strictly aerobic, non-pathogenic bacterium).
- Therapeutic Chassis: Escherichia coli BL21(DE3) or an E. coli-based cell-free protein synthesis (CFPS) platform.
Inputs, Biological Processes, and Outputs
Inputs:
- Culture Broth: Modified Hestrin-Schramm (HS) medium consisting of glucose (20 g/L) or locally refined cane sugar, peptone (5 g/L), yeast extract (5 g/L), disodium phosphate (Na2HPO4, 2.7 g/L), and citric acid (1.15 g/L), adjusted to pH 5.0.
- Biotemplate Mold: A negative truncated cone matching the patient’s residual limb, 3D-printed in PETG/PLA with gas-permeable sidewall micropores.
- Peptide Expression Elements: Terrific Broth growth medium, IPTG chemical inducer, and an expression plasmid encoding an antimicrobial peptide (Magainin-2 or Dermcidin derivative) fused to a Cellulose-Binding Domain (CBD).
Biological Processes:
- Membrane-bound cellulose synthase complexes in K. xylinus polymerize UDP-glucose into linear beta-1,4-glucan chains.
- Extruded microfibrils crystallize and self-assemble into a coherent, 3D nanofibrillar pellicle along the air-liquid boundary within the 3D-printed mold.
- Concurrently, E. coli expresses the hybrid AMP-CBD fusion protein under the control of the T7 promoter upon IPTG induction.
Outputs and Post-Processing:
- The harvested raw cellulose sleeve is treated in 0.5 M NaOH at 80°C for 60 minutes to eliminate bacterial biomass and endotoxins, producing an acellular white scaffold.
- The scaffold is neutralized, washed with sterile water, and incubated in an 8% v/v glycerol solution to achieve elastomeric flexibility.
- The plasticized sleeve is immersed in the recombinant peptide solution; the high-affinity CBD tag anchors the antimicrobial peptides across the nanofibrils without blocking their bactericidal action.
(3) How would you use automation?
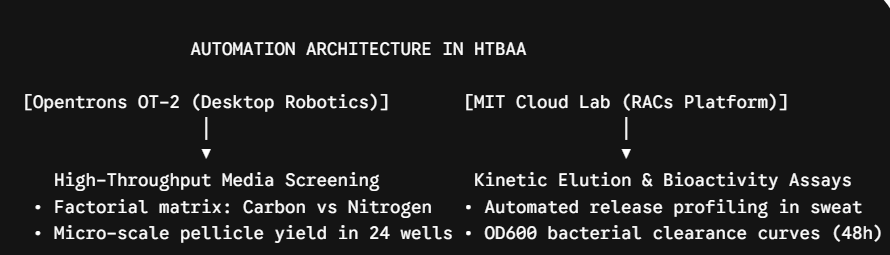
Automation will address process bottlenecks across two key stages: desktop liquid handling and cloud lab screening.
1. Media Formulation Optimization via Desktop Liquid Handling (Opentrons OT-2)
- Workflow: Optimization of growth kinetics and pellicle density.
- Automation Implementation: An Opentrons OT-2 robot will execute Design of Experiments (DoE) protocols in 24-deep-well plates. The system will systematically dispense varying ratios of carbon sources (analytical glucose vs. low-cost agricultural molasses), nitrogen levels, and organic buffers. Automated periodic optical density and dry-weight measurements will identify the fastest pellicle assembly conditions without manual pipetting errors.
2. Elution Kinetics and Bioactivity Assays in the MIT Cloud Lab
- Workflow: Verifying peptide retention and antimicrobial stability under continuous contact with human perspiration.
- Automation Implementation: Using the Reconfigurable Automation Carts (RACs) within the MIT Cloud Lab, standardized cellulose discs functionalized with fluorophore-tagged peptides will be exposed to simulated sweat (saline buffer, pH 5.5). Automated robotic arms will transfer wash fractions to plate readers every 30 minutes over a 48-hour schedule to track peptide release rates, while scheduled inoculations against challenge strains (S. aureus) will quantify clearance kinetics via automated OD600 spectrophotometry.
(4) How much would you need to make, and how long would it take?
(a) How Much? (Scale Definition & Calculations)
The target production scale is a pilot clinical batch to equip 100 transtibial amputees (N = 100) at a regional orthopedic center.
Anatomical Parameters (Per Bio-Liner):
- Geometry: Closed-end hollow truncated cone
- Proximal radius (r1): 6.0 cm
- Distal radius (r2): 4.0 cm
- Vertical height (h): 25.0 cm
- Hydrogel wall thickness (t): 0.5 cm (5 mm, clinical cushioning standard)
Surface Area and Volume Calculations:
Slant height (g):
- g = sqrt(h² + (r1 - r2)²)
- g = sqrt(25² + (6 - 4)²) = sqrt(625 + 4) = sqrt(629) = 25.08 cm
Lateral Surface Area (A_lat):
- A_lat = π × (r1 + r2) × g
- A_lat = 3.1416 × (6 + 4) × 25.08 = 787.9 cm²
Distal Base Area (A_base):
- A_base = π × r2² = 3.1416 × (4)² = 50.3 cm²
Total Surface Area (A_total):
- A_total = 787.9 cm² + 50.3 cm² = 838.2 cm² (approx. 0.084 m²)
Required Hydrogel Volume per Liner:
- V_liner = A_total × thickness
- V_liner = 838.2 cm² × 0.5 cm = 419.1 cm³ (approx. 0.42 Liters)
Biomass and Active Agent Requirements:
Fresh bacterial cellulose hydrogel consists of ~1.5% w/v dry cellulose and 98.5% water:
- Dry cellulose per unit = 419.1 g × 0.015 = 6.29 g
For the full batch of 100 patients:
- Total dry cellulose required: 100 × 6.29 g = 629 g (approx. 0.63 kg)
- Total hydrated hydrogel volume: 100 × 0.42 L = 42 Liters
Antimicrobial peptide requirements (target surface density: 15 µg/cm²):
- AMP per unit = 838.2 cm² × 15 µg/cm² = 12,573 µg = 12.6 mg
- Total purified AMP for 100 units: 100 × 12.6 mg = 1.26 g of peptide
(b) How Long? (Manufacturing Timeline & Throughput)
1. Bacterial Cellulose Synthesis Kinetics (K. xylinus)
- Under optimized static culture at 30°C, K. xylinus generates pellicle thickness at approximately 0.8 mm per day.
- Growth time to reach 5 mm thickness:
- 5.0 mm / (0.8 mm/day) = 6.25 days (approx. 7 days / 1 week per batch)
2. Parallel Bioreactor Production
- Operating a modular bank of 15 custom 3D-printed molds simultaneously:
- Batches needed: 100 units / 15 units per batch = 6.67 -> 7 production cycles
- Total cultivation time: 7 batches × 7 days = 49 days (7 weeks)
3. Recombinant Peptide Synthesis (E. coli)
- Standard benchtop expression in E. coli yields between 0.5 g/L and 1.0 g/L of target protein.
- To produce the required 1.26 g of AMP, a single 3-Liter working volume batch in a 5 L benchtop bioreactor yields approx. 1.8 g of protein.
- Fermentation and affinity purification take 48 hours (2 days), conducted during Week 1.
| Manufacturing Phase | Operational Duration | Infrastructure Used |
|---|---|---|
| Phase 1: Peptide Synthesis & Purification | 2 days (Week 1) | 5 L benchtop fermenter + chromatography column |
| Phase 2: Parallel Cellulose Culture | 7 weeks (Weeks 1–7) | 15 parallel 3D-printed molds in incubator bank |
| Phase 3: Chemical Clearing & Functionalization | 1 week (Week 8) | NaOH clearing bath, glycerol wash, AMP immersion |
| Total Turnaround Time | ~8 weeks | Pilot batch of 100 finished liners |
(5) What don’t you know yet? (Technical Unknowns & Bottlenecks)
Three primary engineering uncertainties require experimental resolution:
Interlaminar Delamination under Multiaxial Dynamic Shear:
Bacterial cellulose possesses high in-plane tensile strength, but its layered fibril deposition makes it susceptible to shear-induced delamination. In a prosthetic socket, cyclic gait causes significant vertical compression combined with rotational and shear stresses. Universal mechanical testing (tensile, compression, and peel tests after 100,000 cycles) is required to ensure the plasticized hydrogel will not separate during regular walking.Oxygen Depletion across Deep Vertical 3D Profiles:
K. xylinus is an obligate aerobe that preferentially synthesizes cellulose at the air-liquid boundary. In a vertical conical cavity 25 cm deep, oxygen diffusion into the lower regions is naturally restricted. Without intervention, this gradient would cause non-uniform wall thickness, resulting in a thin, fragile distal end. We need to experimentally determine whether gas-permeable silicone microporous mold walls provide sufficient passive aeration or if forced micro-perfusion is required.Peptide Immobilization Durability in Acidic Human Sweat:
Human perspiration contains salts (NaCl), urea, and lactic acid at pH levels between 4.5 and 6.5, alongside native skin proteases. It remains to be determined whether physical affinity binding via the Cellulose-Binding Domain (CBD) is robust enough to prevent rapid washout during heavy sweating, or if chemical covalent crosslinking (such as EDC/NHS coupling) will be necessary to ensure long-term antimicrobial protection.
AI Disclosure and Attribution
- Tool: Google Gemini (Fall 2026 Interactive Bioengineering Assistant).
- Scope of Assistance: Used for brainstorming cross-disciplinary connections between FDM 3D printing, medical devices, and biomanufacturing; structuring back-of-the-envelope volumetric and mass yield equations; referencing growth parameters for K. xylinus and E. coli; and translating/formatting the proposal to match all five required questions of HTBAA Homework #1.